
Section: FoodTechX · Tech Insight
Simultaneous push notification: Official WeChat account of Boyuan Information Technology (Guangzhou) Co., Ltd.
Target audience: Purchasing decision-makers, technical directors, equipment engineers, project managers, and technical personnel from equipment manufacturers in food processing plants.
I. Introduction: Acceptance is a systematic inspection of the entire project chain.
In procurement projects for aseptic blow-fill-seal (BFC) production lines, the acceptance phase is often the most contentious and prone to disagreements. No client would underestimate the importance of acceptance for a production line costing tens of millions, yet in practice, delays, disputes, and even project shelving frequently occur.
The root cause often lies not in the "acceptance attitude", but in the "preparation and knowledge required for acceptance". Many clients underestimate the preparatory work they need to complete before acceptance—is the factory cleanliness up to standard? Are the utilities adequate? Are the material parameters accurately defined? Is the operating team in place? These seemingly external conditions are precisely the key to a smooth acceptance process.
On the other hand, insufficient pre-procurement assessment is also a significant contributing factor to acceptance conflicts. If the client lacks a clear definition of its product needs, production capacity targets, and packaging specifications during the bidding stage, or if there is insufficient communication regarding acceptance standards and responsibility boundaries during technical negotiations, these issues will inevitably surface during the acceptance phase.
This article aims to provide purchasers, technicians, business owners, and equipment manufacturers with a complete knowledge system for aseptic production line acceptance. It helps all parties gain a clear understanding of the entire acceptance process from the outset of the project, thereby reducing disagreements and improving project delivery efficiency. When all parties reach a consensus on standards, methods, and boundaries of responsibility, acceptance ceases to be a game of negotiation and becomes a shared confirmation of the project's outcome.
II. Project Initiation: A clear understanding of the client's needs is a prerequisite for acceptance.
Before discussing any acceptance criteria, we must first answer one question: What exactly does the client want to produce?
2.1 List of Requirements Defined by Party A
|
Demand Categories |
Specific content |
illustrate |
|
Product Positioning |
What types of products do you produce? (Acidic/Neutral/Gas-containing/Particulate-containing) |
The configuration level of the sterile line is determined. |
|
Production capacity target |
Peak capacity (BPH), average daily output, annual output |
Influences equipment selection and the scale of supporting public works. |
|
Quality Standards |
Target market (domestic/export), certification requirements (BRCGS/FDA/FSSC 22000) |
Determine the verification level and documentation requirements |
|
Nutrition and flavor preservation |
Requirements for flavor retention and vitamin retention of the contents |
Affecting UHT temperature selection and filling temperature setting |
|
Filling accuracy |
Volume accuracy, liquid level accuracy |
Implement in accordance with the relevant clauses of GB/T 41124-2021 |
|
Packaging specifications |
Bottle shape (round/square/irregular shape), bottle mouth (PCO1881/38mm), capacity (150ml–1250ml) |
Influences the design of blow molds and filling valves, as well as the concentration and duration of the sterilization solution. |
|
Budget range |
Total equipment investment and operating cost affordability |
Influences on import/domestic choices and technical solutions |
|
Delivery cycle |
Time requirement from signing the contract to starting production |
Impact on project planning and acceptance schedule |
Note : For turnkey projects, the technical requirements for labels (adhesive/sleeve labels/heat shrink), paper film packaging, palletizing, automatic control and information systems (MES interface, batch traceability) must be specified in the subsequent processes. These will be considered in the overall acceptance and will not be discussed in this article.
2.2 Material Technical Requirements
The acceptance of sterile production lines depends on the accurate definition of the materials. The client must clearly provide the following material parameters:
|
Material parameters |
Requirements |
Impact on acceptance |
|
pH value |
Acidic (≤4.6) / Neutral (>4.6) |
Determine the aseptic cycle requirements (acidic ≥72h, low acidic ≥48h). |
|
Viscosity |
Low viscosity (e.g., water) / Medium viscosity (e.g., juice) / High viscosity (e.g., concentrated juice / dairy products) |
Impacts filling valve design and CIP cleaning difficulty |
|
Particle content |
Does it contain fruit pieces/fiber/nut pieces? What is the maximum size of the pieces? |
Influences on filling valve selection and sterilization method |
|
Thermosensitive |
Is it temperature sensitive (e.g., NFC juice/plant protein)? |
Affecting UHT temperature selection and filling temperature setting |
|
Bubble tendency |
Does it foam easily (e.g., plant proteins containing saponins)? |
Affects filling speed and liquid level control |
2.3 The Importance of the Microbiological Characteristics of Materials
A thorough understanding of the microbiological characteristics of materials is a prerequisite for designing aseptic processes and determining acceptance criteria. The client should fully communicate the following information with the equipment supplier:
Common types of contaminating bacteria:
- Thermophilic bacteria (such as Geobacillus stearothermophilus ): commonly found in dairy products and plant protein beverages, heat-resistant, and one of the standard indicator bacteria commonly used in UHT sterilization and Media Fill testing.
- Psychrophilic bacteria (such as Pseudomonas fluorescens ): commonly found in raw materials stored under cold conditions, and may multiply at low temperatures.
- Yeasts and molds : commonly found in fruit juices and sugary drinks, they are relatively resistant to acid.
- Lactic acid bacteria : commonly found in fermented beverages or raw materials that have not been fully sterilized.
- Bacillus (such as Bacillus subtilis ): widely found in raw materials and the environment, with strong heat resistance.
Sources and pathways of pollution:
- The raw materials themselves carry : spores in dairy raw materials, yeast/mold in fruit juice raw materials.
- Cross-contamination during production : dead zones in pipelines, valve leaks, incomplete CIP (Continuous Injection Processing).
- Environmental factors : Insufficient cleanliness in the filling area; unprofessional conduct by operators.
- Packaging material contamination : Preforms/caps become contaminated during transportation or storage.
The logic behind choosing sterilization temperature and method:
- Acidic materials (pH≤4.6) : Generally, UHT sterilization at 95-105℃ is used. The low pH inhibits spore germination, and relatively mild sterilization conditions can be adopted.
- Neutral materials (pH>4.6) : Must be sterilized using UHT at 135-145℃ for 2-5 seconds to ensure spores are killed.
- High-protein/high-fat materials : require appropriately extended sterilization time or increased temperature to ensure uniform heat penetration.
- For materials containing particulate matter : the sterilization effect at the center temperature of the particles needs to be considered, which may require higher temperatures and longer holding times.
Key principle : Accurate understanding of the microbiological characteristics of materials directly determines the design of the sterilization process and the setting of acceptance criteria. The client should provide microbiological testing reports for the raw materials (such as spore count and thermostable bacteria count) as one of the bases for equipment design and acceptance.
III. Core Standards System: The Legal Basis for Acceptance
3.1 Specific Standards (Directly Applicable)
|
Standard Number |
Standard Name |
state |
Scope of application |
|
GB/T 41124-2021 |
General Technical Requirements for Aseptic Blow-Fill-Switch Integrated Machine |
Current (effective July 1, 2022) |
The most core national standard specifies the terminology, parameters, technical requirements, test methods, and acceptance-related content. |
|
GB/T 24571-2009 |
Aseptic Cold Filling Production Line for PET Bottles |
in force |
Traditional aseptic cold filling lines are still being used as a reference. |
|
GB/T 33467-2016 |
General Technical Requirements for Fully Automatic Blow Molding, Filling, and Capping Machines |
in force |
Non-sterile but applicable general mechanical requirements for blow-fill-seal integrated machines |
3.2 Group Standards (Industry Best Practices)
- T/CLIMA 002-2021 "Acceptance Specification for Aseptic Blow-Fill-Switch Integrated Machine" – This standard clarifies for the first time the specific indicators and methods for aseptic validation.
- T/CLIMA 003-2021 "PET Bottle Aseptic Blow-Fill-Switch Integrated Machine" - Specifically designed for the special requirements of carbonated beverages.
- T/CFPMA 0020-2021 "Aseptic Validation Specification for Aseptic Filling Production Line of PET Bottles" provides a complete validation process template.
Note : Group standards become legally binding upon adoption as stipulated in procurement contracts or technical agreements. It is recommended that the tender documents explicitly require suppliers to commit to complying with the aforementioned group standards.
IV. Division of Responsibilities: What the Client Does, and What the Equipment Supplier Does
This is the area most prone to disputes during the acceptance process, and it must be clearly defined before the contract is signed.
4.1 Scope of Responsibilities of Party A (Purchaser)
|
Responsibilities |
Specific content |
Corresponding standards/requirements |
|
Factory buildings and cleanrooms |
Provide a compliant factory building; the filling area must meet ISO Class 5 (Class 100) standards. |
GB 50073 Cleanroom Design Code |
|
Food production licensing conditions |
Obtain a food production license and establish a HACCP system. |
GB 14881 General Hygiene Standard for Food Production |
|
Public works supporting facilities |
Steam, compressed air, purified water, cooling water, electricity, etc. |
In accordance with the utility conditions sheet provided by the equipment supplier. |
|
Raw material preparation |
Food-safe PET preforms, caps, and materials |
GB 4806.1 General Requirements for Food Contact Materials |
|
Operations Team |
Equipped with trained operation and maintenance personnel |
The equipment supplier provides training, and the client's responsible personnel are in place. |
Clearly define the boundaries : Standards such as GB 14881 and GB 50073 are basic requirements that the client must meet during the factory construction phase and are not within the scope of the equipment supplier's supply. The equipment supplier's obligation is to deliver a sterile production line conforming to GB/T 41124-2021, provided that the client provides qualified factory buildings and utilities.
4.2 Scope of Responsibilities of Equipment Manufacturers (Suppliers)
|
Responsibilities |
Specific content |
Corresponding standards/requirements |
|
Equipment design and manufacturing |
BFC all-in-one machine designed and manufactured according to the technical specifications agreed in the contract. |
GB/T 41124-2021 |
|
Aseptic verification |
Perform a culture medium filling challenge test to demonstrate aseptic assurance capability. |
T/CLIMA 002-2021 |
|
Installation and debugging |
Complete equipment installation, commissioning, and integrated testing at the client's site. |
According to the installation plan confirmed by both parties |
|
Training |
The client's operation and maintenance personnel shall receive no less than four weeks of training. |
The training plan is attached to the contract. |
|
Technical document delivery |
Provide equipment drawings, operation manuals, maintenance manuals, and verification reports. |
List of documents stipulated in the contract |
4.3 The Role of Third-Party Organizations
For aseptic validation, it is recommended to engage a third-party testing organization with CMA/CNAS accreditation (such as SGS, TÜV, CTI, Intertek, etc.) to conduct independent verification and issue a report. The role of the third party is:
- Witness the entire process of culture medium filling and testing
- Independent testing of environmental microorganisms
- Issue a legally valid verification report (for BRCGS/FDA audits).
- Provide impartial judgment when there is a dispute between Party A and Party B regarding the verification results.
V. Technical Level of Aseptic Lathes: A Four-in-One Approach to Structure, Materials, Manufacturing, and Management
The technical level and quality of sterile sutures cannot be measured by a single parameter, but are determined by the following four aspects:
5.1 Structural Design and Working Principle
Good sterile sutures first and foremost stem from excellent structural design and working principles:
- Aseptic area isolation design : positive pressure maintenance, airlock transition, dynamic sealing technology
- The rationale for choosing a sterilization method : H₂O₂ dry method vs. PAA wet method .
- CIP/SIP System Design : Cleaning Coverage, Dead Zone Elimination, Turbulence Protection
- The filling valve is designed to be drip-free, easy to clean, and provides a sterile barrier.
- The design of the conveyor system should ensure smooth transitions, reduce friction, and prevent secondary contamination.
Key takeaway : Structural design determines the inherent characteristics of a sterile suture. No amount of skillful operation can compensate for a poorly designed machine.
5.2 Selection of Materials and Key Components
The choice of materials directly determines the durability, hygiene, and operational stability of the sterile liner:
|
Component Category |
Recommended materials/brands |
Effect on sterile line level |
|
Metal materials in contact with other materials |
304/316L stainless steel, surface roughness Ra≤0.8μm |
Corrosion resistant, easy to clean, and does not produce a metallic taste. |
|
Seals |
EPDM (Ethylene Propylene Diene Monomer) / FKM (Fluororubber), compliant with FDA/USP Class VI |
High temperature resistance, acid and alkali resistance, and no foreign matter precipitation. |
|
Transmission components |
Servo motors (such as Siemens/Schneider/Huichuan), precision gear reducers (SEW/Guomao/ Jiepai / Sankai ) |
High changeover accuracy, stable operation, and low energy consumption |
|
Sensor |
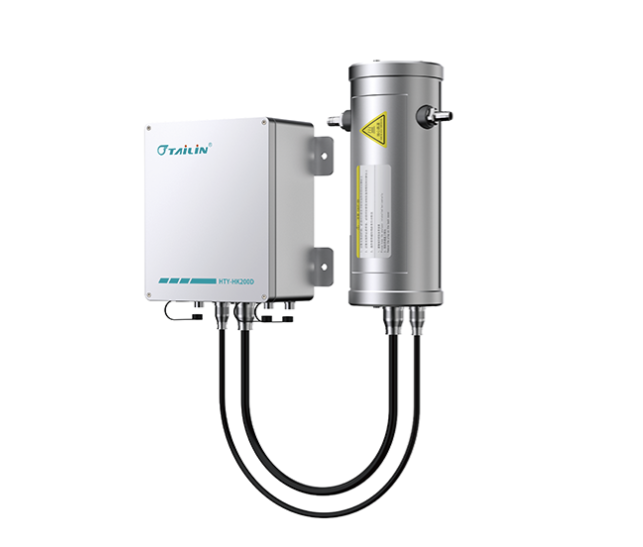
Liquid level sensors, pressure sensors, temperature sensors, and dynamic testing sensors for sterile atomized environments(such as Endress+Hauser/WIKA/Tylene). |
Reliability of filling accuracy, aseptic environment monitoring, and atomization effect verification |
|
Electrical components |
PLCs (Siemens/Mitsubishi/Rockwell), frequency converters, low-voltage electrical appliances |
Stability and scalability of the control system |
|
Standard parts |
Bolts, nuts, and washers (made of stainless steel and meeting food-grade requirements). |
Anti-loosening, easy to disassemble and clean, with no dead corners for hygiene. |
|
Pneumatic components |
Cylinders, solenoid valves, and pneumatic fittings from brands such as Festo, SMC, and AIRTAC. |
Reliable operation, fast response, and easy maintenance |
Key principle : Good design requires good materials and components. Even with the most advanced design, a sterile production line cannot guarantee long-term stable sterile production if it uses inferior seals or stainless steel.
5.3 Industrial Manufacturing System
Good design also requires advanced manufacturing equipment to ensure its success. The machining of high-precision components depends on:
- Five-axis machining center : used for high-precision machining of complex molds and valve bodies.
- Gantry milling /Large CNC milling machine : Used for precision machining of machine frames and large structural parts.
- Laser cutting/welding equipment : used for precision forming and seamless welding of sheet metal parts.
- Appearance and physicochemical testing instrument : used for dimensional inspection and material analysis of parts.
Production process inspection should include: welding quality (argon arc welding/rail welding), surface roughness (Ra≤0.8μm), precision of machine parts, and assembly accuracy. In addition, a comprehensive quality management system (such as ISO 9001 certification) and a proper outgoing inspection process are required.
5.4 Management and Execution Team
Even the best equipment needs people to operate and maintain it.
- Equipment vendor team : Project management capabilities, installation and commissioning experience, and after-sales service response speed.
- The client's team : Operators' basic microbiological knowledge, maintenance personnel's mechanical and electrical skills, and management's quality awareness.
- Training and handover : A complete training plan, operating procedures (SOPs), and emergency response drills.
In short : The quality of a sterile production line = structural design × material selection × manufacturing quality × team capability. All four are indispensable.
VI. Acceptance Method: How to determine if it passes?
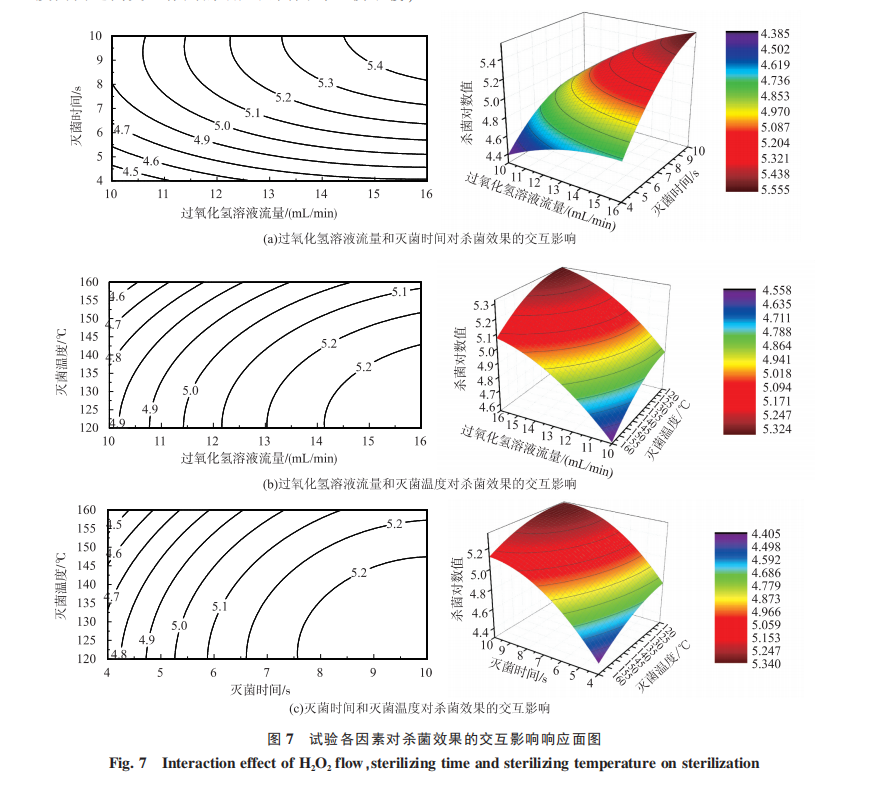
6.1 Four Dimensions of Acceptance
A complete aseptic validation must cover the following four dimensions:
- Material sterility validation : Confirm that the UHT-sterilized materials meet commercial sterility requirements.
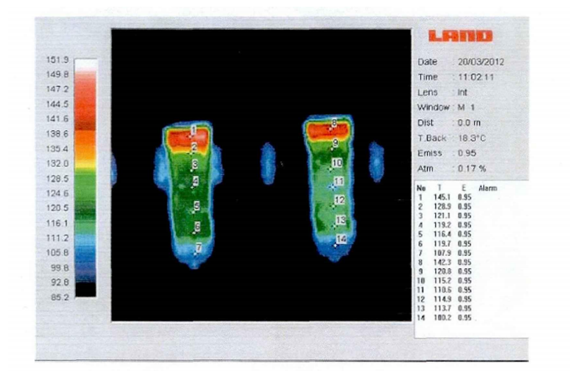
- Packaging material aseptic validation : confirming that the preforms and caps achieve the required sterilization efficiency after sterilization.
- Environmental aseptic validation : Confirm that the cleanliness of the filling area meets ISO Class 5 (Class 100) requirements.
- Equipment sterility validation : Confirm that the CIP/SIP system can maintain a sterile state inside the equipment.
6.2 Overview of Key Acceptance Indicators
|
Validate Project |
Qualification Standard |
Brief description |
|
Commercial Sterility Assurance Level (SAL ) |
≤10 ⁻⁶ |
Challenge tests were conducted using standard indicator bacteria of thermoresistant Bacillus species, and the results were repeatedly verified. |
|
Continuous aseptic running time (neutral product ) |
≥72 hours (Pass); ≥120 hours (Excellent) |
Regular sampling and testing during continuous operation |
|
Continuous aseptic running time (acidic products ) |
≥72 hours |
Same as above |
|
H₂O₂ residue |
≤0.5 mg/L |
Test according to GB 5009.226 method |
|
Cleanliness of the filling area |
ISO Class 5 (100-level) |
Test according to GB/T 16292/16293/16294 |
|
Sterilization efficiency of bottle preform/cap |
Inner surface SE≥5, outer surface SE≥4 |
A comprehensive judgment was made using methods such as staining tests and microbial patch tests. |
|
Production efficiency |
≥95% |
Continuous operation statistics |
|
Finished product qualification rate |
≥99.5% |
Comprehensive inspection of appearance, filling accuracy, and sealing performance. |
Note: Due to the significant differences in material categories and usage scenarios, the specific acceptance criteria shall be subject to the agreement between both parties.
6.3 Basic Principles of Media Fill Test
Culture medium filling tests are the most convincing method for aseptic validation, and their core principles include:
- Simulate actual production : Use growth-promoting culture medium instead of the product to simulate the entire normal production process (including changes in type, interruptions, etc.).
- Covering the aseptic cycle : Sampling was conducted at the beginning, middle, and end of the aseptic operation cycle.
- Sufficient sample size : The number of bottles sampled each time should be sufficient to statistically demonstrate that the contamination rate is below the set acceptable standard.
- Cultivation and Observation : After filling, the samples were incubated at a suitable temperature for a sufficient number of days, and the microbial growth was checked on each bottle.
- Acceptance criteria : The contamination rate must be below the agreed threshold (usually 1/10,000 or lower).
The specific sampling quantity, time interval, and culture conditions should be specified in detail in the validation protocol based on the equipment capacity, product type, and standards agreed upon in the contract (such as GB/T 41124-2021, T/CLIMA 002-2021).
6.4 Scope of Results and Beyond the Solution
|
situation |
Solution |
|
All qualified |
Signing the acceptance certificate marks the start of the warranty period. |
|
Some indicators did not meet the standards (excluding those listed in the red line ). |
Both parties agreed on a rectification period, and a re-inspection was conducted after rectification. |
|
Aseptic validation failed (contamination rate exceeded the standard ). |
Red-line item : The equipment supplier must identify the cause and rectify it, and re-perform the complete Media Fill Test at the supplier's expense. |
|
Production capacity not up to standard |
The penalty clause stipulated in the contract shall be followed, or a downgraded acceptance shall be negotiated. |
|
H₂O₂ residues exceeded standards . |
Red line item : Equipment manufacturers must optimize sterilization processes until they meet the standards. |
|
Cleanliness level not up to standard (issues with the client's factory ). |
Party A is responsible for rectifying the factory building, and the equipment supplier will cooperate with the retesting. |
6.5 The Red Line That Cannot Be Crossed
The following clauses are veto items ; if any one of them fails to meet the standard, Party A has the right to refuse acceptance:
|
Red line item |
Standard requirements |
reason |
|
Commercial Sterility Assurance Level (SAL) |
≤10 ⁻⁶ |
Food safety bottom line |
|
Product contamination rate |
≤1/10,000 (or the value agreed upon in the contract) |
The fundamental purpose of sterile sutures |
|
H₂O₂ residue |
≤0.5 mg/L |
Food safety and regulatory requirements |
|
Cleanliness of the filling area |
ISO Class 5 |
Basic guarantee of a sterile environment |
VII. Acceptance and coordination of external supporting conditions
The acceptance of sterile lines cannot be carried out in isolation; it must be effectively integrated with external supporting conditions.
7.1 Packaging Material Requirements
Party A shall confirm the following packaging material parameters before acceptance and provide them to the equipment supplier as a basis for commissioning:
|
Packaging parameters |
Requirements |
Acceptance related items |
|
Bottle type and size |
Round/square/irregularly shaped bottles, height/diameter/wall thickness |
Affects blow molding dies, conveying systems, and labeling machines. |
|
Bottle neck specifications |
PCO1881 / 38mm double-ended thread / Other |
Affects filling valve, capping head, and sealing performance |
|
Capacity range |
150ml–1250ml (or larger) |
Affects filling volume setting and changeover parts |
|
Bottle cap type |
PCO1881 / 38mm double-ended thread / gasket / other |
Affects cap torque setting and sealing performance |
|
Tags and back packaging |
Labeling method (self-adhesive/sleeve label/heat shrink), packaging form (film wrap/carton/plastic box) |
Influences the selection and layout of downstream equipment |
7.2 Environmental Requirements
|
Environmental parameters |
Require |
Responsible party |
|
Cleanliness of the filling area |
ISO Class 5 (100-level) |
Party A is responsible for the construction of the factory building. |
|
Pressure difference in clean area |
≥10 Pa in non-clean areas |
Party A is responsible for the HVAC system |
|
Temperature and humidity |
According to product process requirements (usually 20-25℃, RH≤60%) |
Party A is responsible for the air conditioning system |
|
Illumination |
Meets food factory lighting standards |
Party A is responsible |
|
Drain |
Ground slope and drainage ditch design |
Party A is responsible |
7.3 Other supporting facilities
|
Supporting items |
Require |
Responsible party |
|
Steam supply |
Pressure, flow rate, and purity meet the requirements of UHT and CIP. |
Negotiation between the two parties |
|
Compressed air |
Oil-free, dry, and pressure-stable |
Negotiation between the two parties |
|
Power supply |
Voltage, frequency, capacity, stability |
Party A is responsible |
|
Tap water |
Water quality meets process requirements |
Party A is responsible |
|
Cooling water |
Temperature meets process requirements |
Negotiation between the two parties |
|
Purified water |
Water quality meets process requirements |
Equipment vendor responsible |
|
CIP station |
Cleaning agent storage tanks, heating and conveying systems |
Equipment vendor responsible |
|
Environmental protection facilities |
Waste gas/wastewater treatment, etc. |
Negotiation between the two parties |
VIII. Mechanism for handling changes in the circumstances of both parties
During project execution, circumstances may change for both parties, necessitating a pre-agreed handling mechanism:
8.1 Changes in Party A's Requirements
|
Changes |
Solution |
|
Product formulation adjustments (e.g., changing pH from acidic to neutral) |
The aseptic validation protocol needs to be reassessed, which may incur additional validation costs. |
|
Increased demand for production capacity |
Assess equipment capacity; if modifications are needed, a separate agreement will be signed. |
|
Changes in packaging specifications (such as changes in bottle opening/capacity) |
Replacement parts shall be borne by Party A. |
|
Delivery cycle ahead of schedule |
Feasibility assessment may incur expedited fees. |
8.2 Changes in Equipment Supplier Information
|
Changes |
Solution |
|
Key technical parameters cannot meet the standards |
Party A has the right to request a price reduction upon acceptance or to terminate the contract. |
|
Delivery delay |
Execute according to the late payment penalty clause stipulated in the contract. |
|
Change of core component supplier |
Prior written notice and consent from Party A are required. |
8.3 Force Majeure
In the event of project delays caused by force majeure events such as natural disasters, policy changes, or the pandemic, both parties should negotiate amicably to reasonably extend the construction period, which shall not be considered a breach of contract.
IX. Action List for the Purchaser
- Project initiation phase : Complete the "Product and Process Requirements Specification", clarifying material parameters (including microbiological indicators), production capacity targets, and packaging specifications.
- the bidding stage : The technical tender documents should clearly list all applicable standard numbers (GB/T 41124-2021 + T/CLIMA 002-2021 + supporting standards).
- Preliminary Acceptance Test (FAT) : Before the equipment is shipped, Party A shall send personnel to the equipment supplier's factory for a preliminary acceptance test, and conduct spot checks on certain aspects of the production process to confirm the completeness of the equipment's appearance, main functions, and accompanying documentation.
- Contract stage : "Passing GB/T 41124-2021 aseptic validation" will be listed as one of the payment conditions, clearly defining the red lines and handling mechanisms.
- Installation Phase : The supplier is required to provide a complete aseptic validation plan and timeline, and the client will simultaneously complete the construction of the factory and utilities.
- Acceptance phase : Engage a third-party testing agency to conduct independent verification and issue a formal report; if the client is unfamiliar with aseptic line technology, it is necessary to engage a professional consulting firm or technical advisor to assist with the acceptance process.
- After production commences : Establish a regular aseptic environment monitoring system (monthly airborne/settled bacteria testing), and conduct a comprehensive aseptic validation review every six months.
X. Conclusion
A sterile blow-fill-seal production line is not a solo act by the equipment supplier, but a systematic project involving collaboration among the client, the equipment supplier, and a third-party organization. Only when each party clearly understands its own responsibilities and strictly adheres to the standards can a satisfactory result be achieved during the acceptance process.
This article is the second in a three-part series on "In-depth Study of Aseptic Blow-Flush (BFC) Technology".
- Previous article: Technical Roadmap – Answering the question "Why choose aseptic cold filling?"
- This section, "Standards and Acceptance," answers the questions: "How is acceptance conducted? Who is responsible for what? What are the standards?"
- Next article: Investment Decisions – Answering "How much money? How to choose suppliers? How to avoid pitfalls?"
stay tuned.
This article is produced by the FoodTechX Technology Research Center; please contact us for authorization to republish.
Sources of data and insights: publicly available technical documentation from corporate websites, industry journal papers, and interviews with offline equipment manufacturers and end-users. If you have any questions regarding the data or views presented, please contact the editorial team at support@foodtechx.com for clarification or verification.
© Boyuan Information Technology (Guangzhou) Co., Ltd. | www.foodtechx.com